Case Study
02
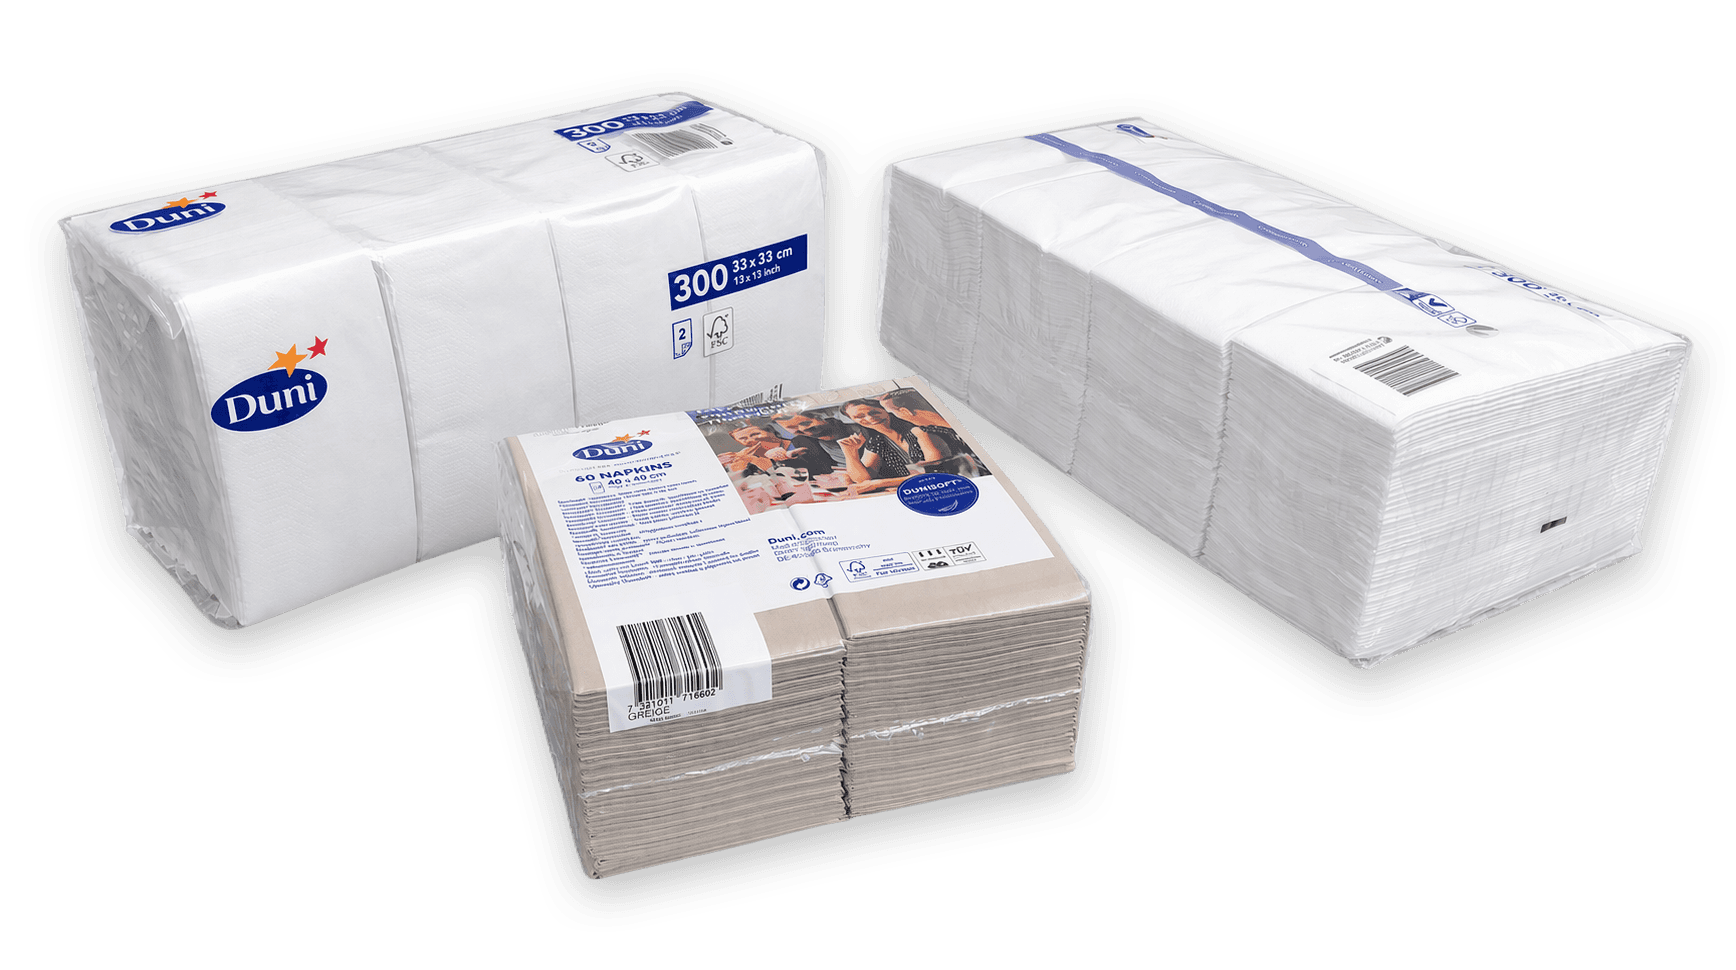
The transfer of the product (film-wrapped napkins) takes place h orizontally flat.
In the infeed, it is positioned from horizontally to vertically or rotated by 90 degrees.
Using a servomotor-driven pusher, the products are grouped acco rding to the
format recipe selected.
Depending on the format, the grouped products can be rotated by 90°.
All products are placed in front of the main pusher by a servom otor-driven lowering movement.
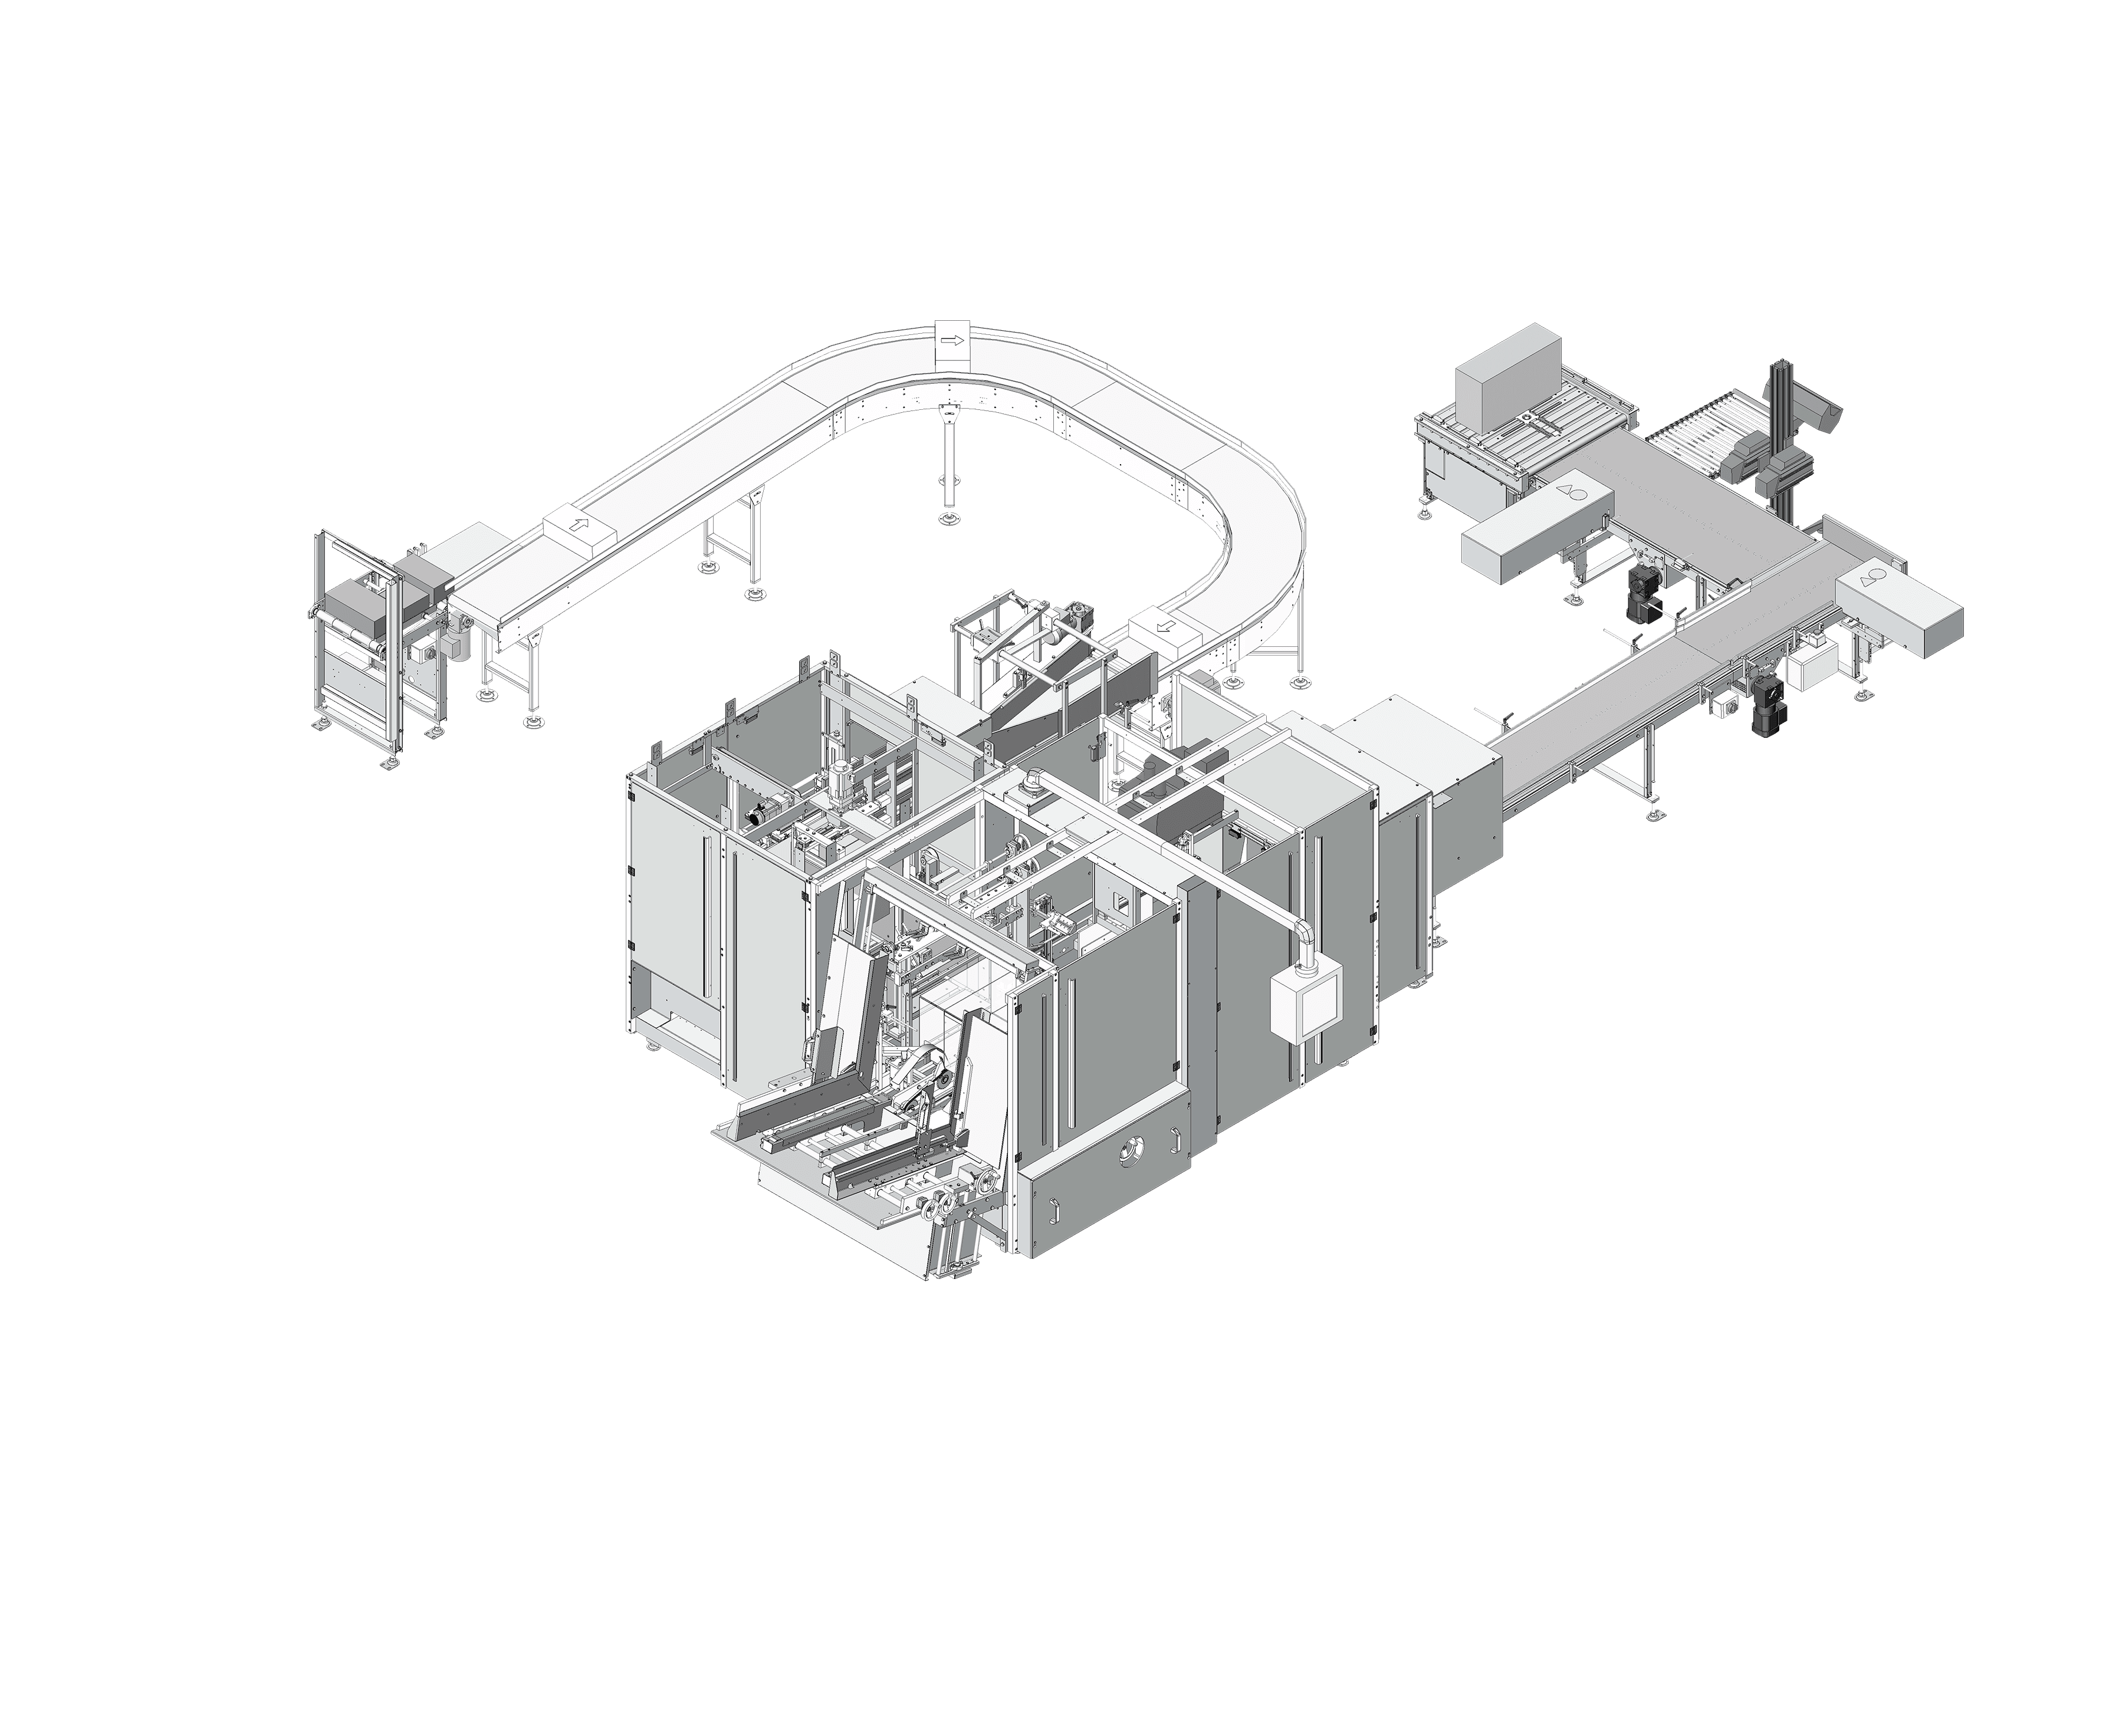
The carton blank is removed from the magazine and positioned in the cycle chain.
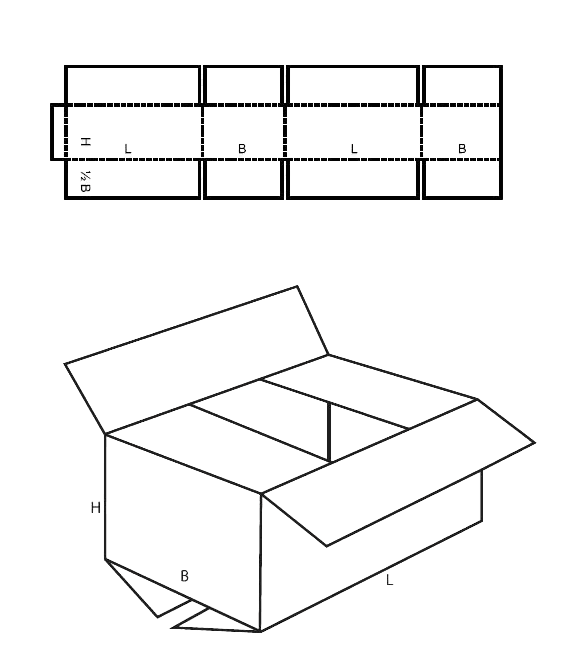
Erecting and filling of the cartons takes place in one station.
The main pusher pushes the grouped products into the carton positioned in the loading station.
The pasting and insertion of the flaps is carried out in the run .
The cartons are then erected while on the outfeed belt.
The cartons are then conveyed to a palletizer.
Servomotor-driven movements of carton removal, cycle chain,
transversal pusher, lowering station and main pusher
All speeds of the conveyor belts can be adjusted infinitely
Forming and filling on one level
All format-dependent parameters can be stored in recipes
Low energy consumption
Minimum protection class IP54
Automatic hot melt refilling system
Outfeed system for individual products and filled cartons
Integrated bar code scanner
Integrated printer
03
| Product Carton | Product dimensions | Formation | Package dimensions | Position in carton | Output |
|---|---|---|---|---|---|
| 214032 (1) | approx. 400 × 200 × 120 mm | 1 × 4 × 1 | approx. 561 × 403 × 211 mm | D 3110288 | 2 carton/min. |
| 171560 (8) | approx. 200 × 200 × 90 mm | 3 × 4 × 1 | approx. 640 × 210 × 360 mm | F 3110362 | 3 carton/min. |
| 214018 (10) | approx. 335 × 165 × 110 mm | 1 × 4 × 1 | approx. 563 × 348 × 175 mm | D 3110293 | 2 carton/min. |

Performance:
Up to 25 cartons/min.